Fused Magnesia Large Crystals: How They Form
- Share
- publisher
- HOLY Magnesium Industry
- Issue Time
- Oct 21,2026
Summary
How large periclase crystals grow in fused magnesia and why size drives refractory performance.
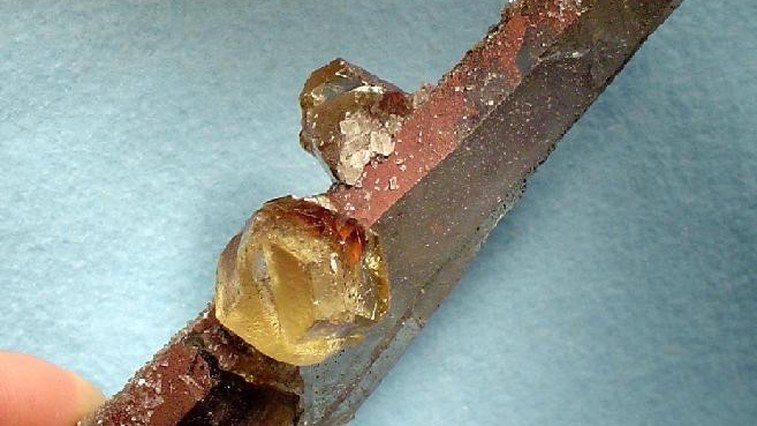
Fused Magnesia Large Crystals: How They Form
Fused magnesia is the premium end of the magnesia family, and what distinguishes it from dead burned magnesia is not simply higher purity but its microstructure. When you break open a piece of fused magnesia you see coarse, glassy periclase crystals, sometimes several hundred micrometres across, rather than the fine, matte grain of a sintered product. Those large crystals are the reason fused magnesia resists slag corrosion so effectively, and they form through a specific and carefully controlled melting and cooling sequence.
From Magnesite to Melt
The process starts with a selected magnesite or a pre-calcined magnesia feed charged into a three-phase electric arc furnace. Arc temperatures exceed 2800 C, well above the roughly 2800 C melting point of pure MgO, so the charge melts completely into a molten bath. Impurities behave differently in the melt: silica, lime, iron oxide and alumina preferentially form silicate phases that are less dense than the periclase melt and that solidify later. This separation is the first purification step and is why the choice of raw feed chemistry matters so much to the final grade.
Crystal Growth During Controlled Cooling
Large crystals are not created in the furnace; they are created during cooling. When power is cut, the bath begins to solidify, and the physics of solidification takes over. Periclase nuclei form first, and because MgO is the majority phase and its melting point is far above that of the silicates, the periclase crystals continue to grow while the surrounding impurity-rich liquid remains molten. The longer the ingot is held at high temperature, the larger the crystals become. This is why fused magnesia ingots are cooled slowly, often over several days, sometimes in insulated pits, rather than quenched.
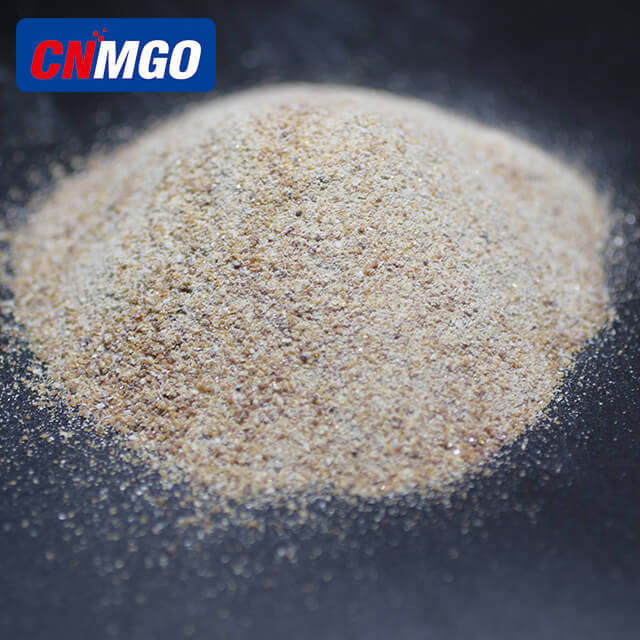
Fused magnesia powder, MgO 95 to 99 percent, milled from large-crystal ingot.
Why Crystal Size Governs Performance
Slag attacks a refractory grain at its boundaries. In a fine-grained sintered product there is a large total area of grain boundary, and the silicate phases sitting there are the weakest, lowest-melting part of the structure; slag infiltrates along them and prises grains loose. In large-crystal fused magnesia there is far less boundary area per unit volume, and the periclase crystals themselves are essentially pure MgO with a melting point near 2800 C. The result is resistance to both chemical dissolution and structural disintegration. Large crystals also mean low apparent porosity and high bulk density, which slows capillary slag penetration.
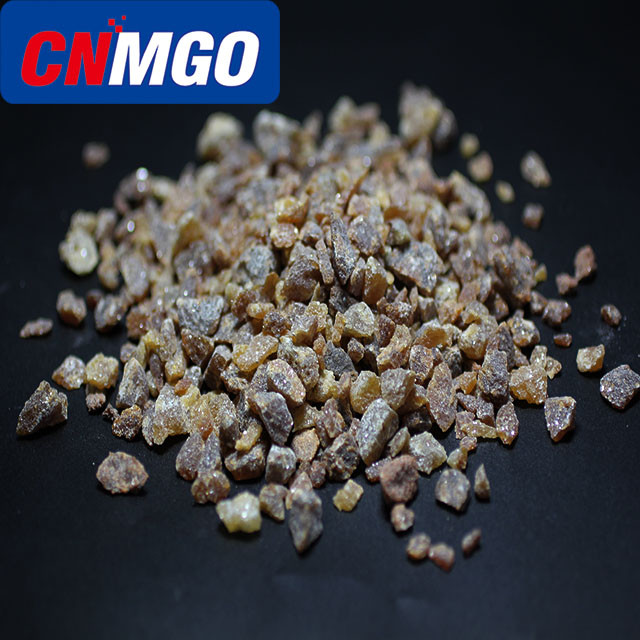
Fused magnesia granular fractions for refractory aggregates and shapes.
Grades and Where the Crystals End Up
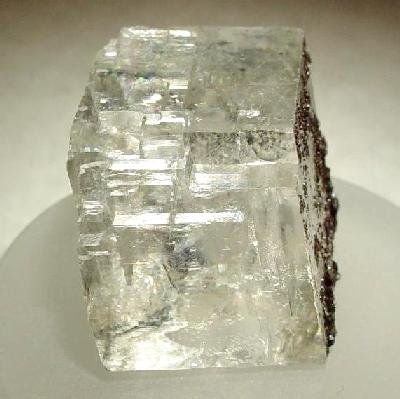
After cooling, the ingot is broken, sorted and crushed, and the degree of sorting determines the grade. The cleanest, best-crystallised core material, often visually identifiable by its large translucent crystals, becomes the highest purity grades at MgO 97 to 99 percent. Material nearer the ingot skin, where impurity silicates have migrated, is graded lower, typically MgO 95 to 97 percent. These fractions are then milled to powder or screened to granular sizes for use in magnesia-carbon bricks, sliding plates, nozzles, crucibles, high-temperature ceramics and electrical heating element insulation.
Specifying Fused Magnesia Sensibly
Buyers should specify MgO content, CaO to SiO2 ratio, bulk density, and where relevant a minimum crystal size or a maximum B2O3 limit, since boron severely depresses the melting point of the bond phase. Grain sizing should be ordered as a matched set of fractions from the same lot so the chemistry is uniform across coarse, medium and fine components. Because fused magnesia carries a real price premium, the disciplined approach is to place it only where corrosion is most severe and to use well-specified dead burned magnesia elsewhere in the same vessel.
Common Misconceptions About Fused Magnesia
Three misunderstandings come up repeatedly. The first is that higher MgO always means better performance; above about 97 percent the marginal gain in corrosion resistance is small, while the CaO to SiO2 ratio and the level of B2O3 often matter more. The second is that all fused magnesia is the same; in practice crystal size and ingot sorting vary between producers and between batches, and the difference shows up in service. The third is that fusion removes impurities, which it does not: fusion redistributes them into the silicate phases that collect at the ingot skin and along crystal boundaries. Selecting on feed chemistry, crystal development and sorting discipline is more reliable than selecting on a headline purity figure alone.
HOLY Perspective
HOLY (CNMGO Group Limited) manufactures fused magnesia at Dashiqiao in Liaoning, controlling furnace charge chemistry and cooling practice to produce consistent large-crystal ingot. Our team can help you match an FM grade and grain set to the corrosion conditions in each vessel position.